
Sinoright Blog
Acetophenone: Technical Specifications & Industrial Appl
As a dual-functional aromatic ketone raw material, acetophenone serves both as a high-boiling solvent for polymer systems and as a core building block for organic synthesis. It directly addresses common industrial pain points such as poor coating leveling, short fragrance retention, and low synthesis yield. We provide two standardized purity grades to match different precision requirements of production lines, with stable batch quality and full supporting documentation to meet the procurement needs of coatings, fragrances, pharmaceuticals and general industrial customers.
Core Grade Specification Comparison
We supply two mainstream commercial grades, differentiated by purity, impurity control and chroma index. The table below lists key technical parameters for direct grade matching.
| Parameter | Industrial Grade | High Purity Grade |
| Purity (GC) | ≥ 99.0% | ≥ 99.5% |
| Moisture | ≤ 0.15% | ≤ 0.08% |
| Appearance | Colorless to pale yellow transparent liquid | Colorless transparent liquid |
| Boiling Point | 202°C | 202°C |
| Typical Application | General coatings, rubber processing, bulk industrial solvents | Fragrance synthesis, pharmaceutical intermediates, fine chemical production |
Core Industrial Application Values
High-Boiling Co-Solvent for Coatings & Resins
As a high-boiling slow-evaporating solvent, acetophenone is widely used in nitrocellulose varnishes, alkyd resin coatings and ink systems. It effectively extends the wet film leveling time, reduces surface defects such as pinholes and orange peel, and improves the gloss and fullness of the coating film. Compared with low-boiling ketone solvents such as acetone and butanone, it has stronger dissolving power for special resins such as cellulose acetate and is more suitable for high-performance coating systems with strict requirements on film appearance.
Fixative & Synthetic Precursor for Fragrance Industry
Acetophenone has a persistent sweet hawthorn-like floral aroma. It is used as a fixative in soap fragrances and industrial flavors to prolong fragrance retention and enrich the fragrance hierarchy. It is also a core precursor for the synthesis of phenylethanol, phenylacetate and other floral fragrances. High purity grade is required for fragrance production to avoid odor deviation caused by trace impurities.
Intermediate for Pharmaceutical & Fine Chemical Synthesis
In the pharmaceutical industry, it participates in the synthesis of choleretic drugs, antipyretic analgesics and other active ingredients; in the fine chemical industry, it is used to produce photosensitizers, antioxidants and dye intermediates. The high-purity grade effectively reduces side reactions in the synthesis process, improves product yield and purity, and reduces the pressure of subsequent purification processes.
General Industrial Auxiliary Applications
It can also be used as a plasticizer for cellulose plastics, a denaturant for industrial alcohols, and a solvent for rubber processing. It has wide industrial adaptability, and the industrial grade can meet the basic performance requirements with high cost performance.
Grade Selection Decision Framework
- Choose Industrial Grade when: Your production involves general industrial coatings, rubber processing, bulk solvent blending and other scenarios with no strict requirements on chroma and trace impurities. This grade balances performance and cost, suitable for long-term mass procurement.
- Choose High Purity Grade when: Your production involves fragrance blending, pharmaceutical intermediate synthesis, fine chemical production and other scenarios with strict requirements on product odor, reaction yield and impurity content. This grade ensures stable process and high finished product quality.
Storage, Handling & Quality Assurance
Acetophenone is a flammable liquid with a medium flash point. It should be stored in a cool, ventilated warehouse away from fire sources and oxidizing agents. Long-term exposure to air will cause color deepening and peroxide value increase, so sealed storage is required.
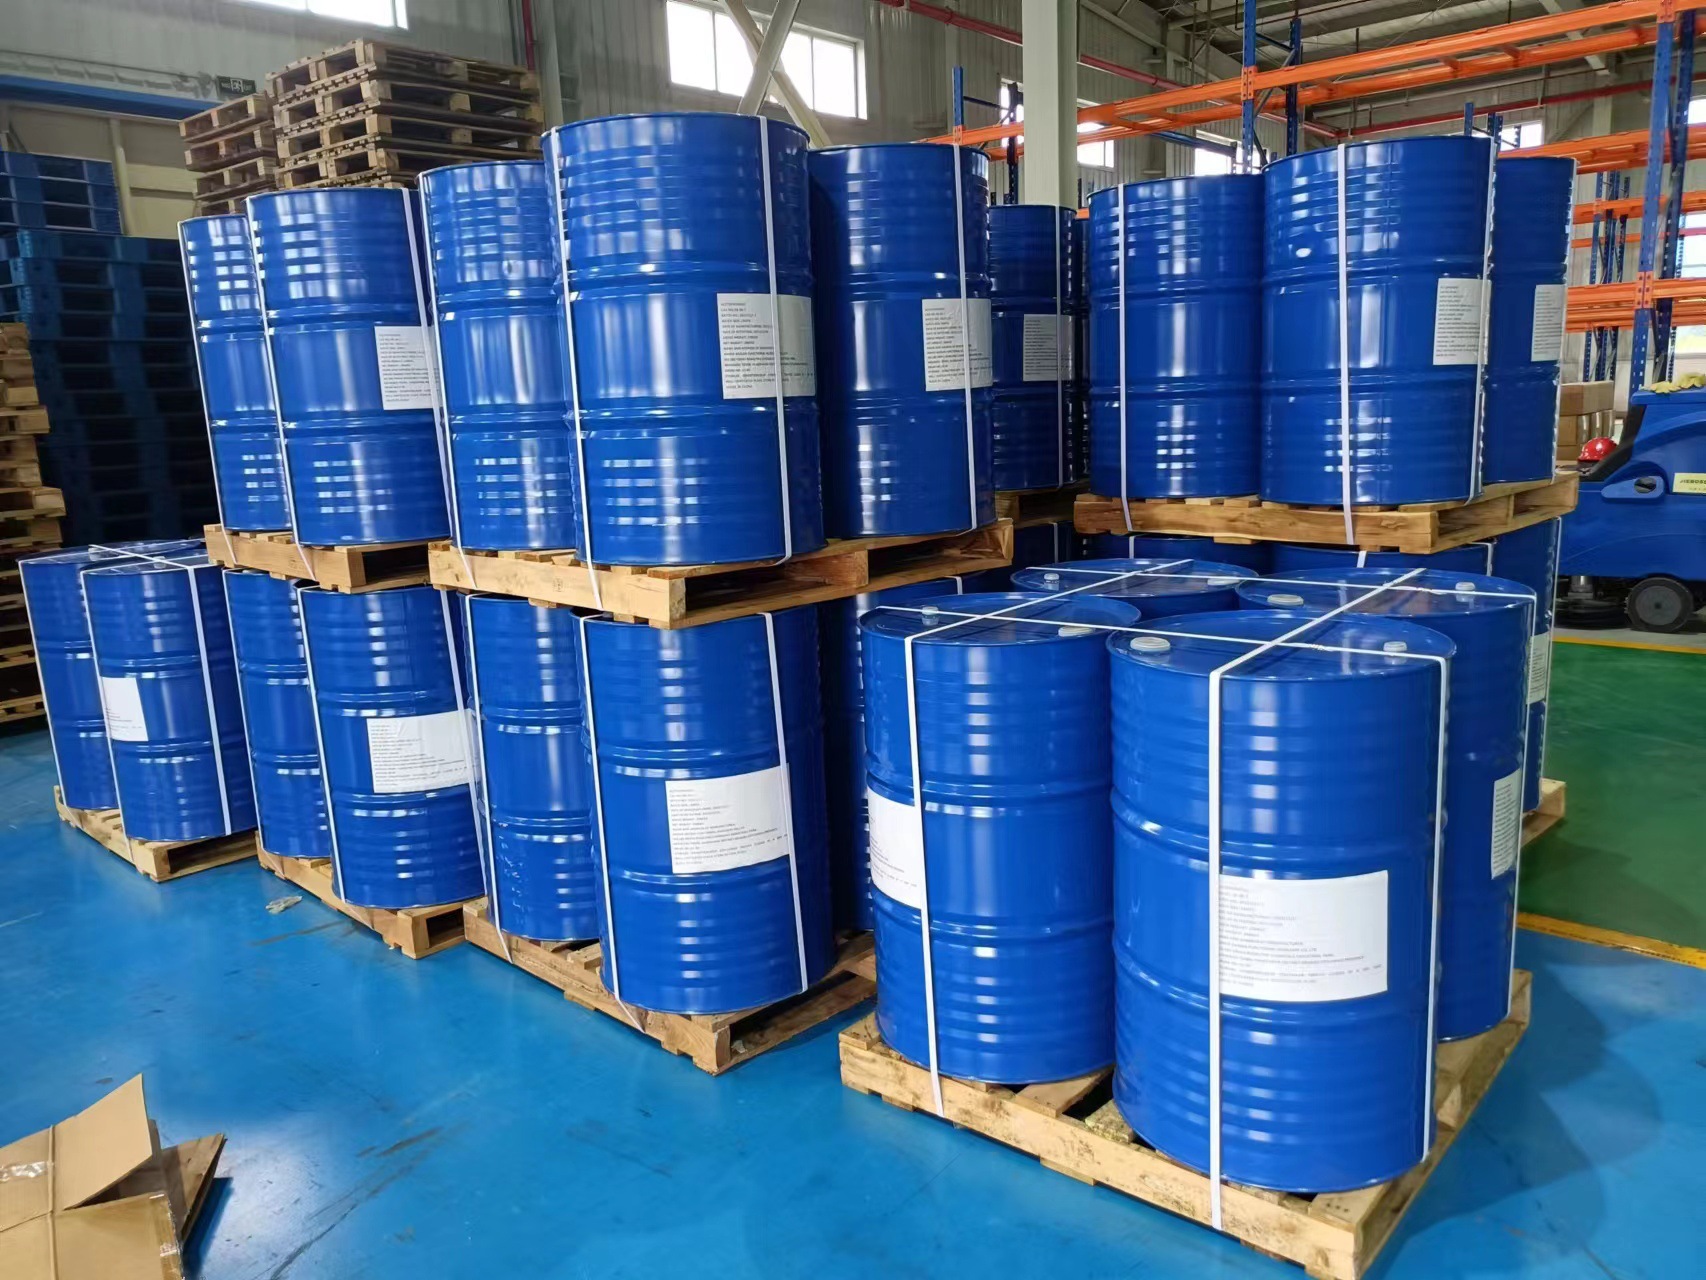
All batches are delivered with complete documents including Certificate of Analysis (COA) and Material Safety Data Sheet (MSDS). Standard 200kg iron drum packaging is available, and customized packaging solutions can be provided according to customer production and logistics requirements.
Technical Q&A
Q1: What is the advantage of acetophenone compared with other high-boiling solvents?
It has both strong dissolving power and good leveling performance. It dissolves more types of resins than ester solvents, and has slower volatilization speed and better film-forming effect than low-boiling ketone solvents.
Q2: Will the color deepening of acetophenone affect use?
Slight color deepening caused by long-term storage does not affect the use as a general industrial solvent. For fragrance and high-end coating scenarios that require chroma, it is recommended to use high-purity grade and use it up within the shelf life.
Q3: Can acetophenone be recovered by distillation?
Yes. It has stable properties and can be recovered and purified by atmospheric distillation in a closed production system, which helps reduce comprehensive production costs.